Webinar Alert! Building Robust Potency Assays with In-Cell Western Assay Protein Expression Readouts Register Today!
Aav Scalaule Suspension Process Optimiz
*PROVEN INTELLIGENCE IN SCALABLE VECTOR PRODUCTION.*
Aav Scalaule Suspension Process Optimiz
CELL & GENE | RNA | BIOLOGICS
AAV Scalable Suspension: Process Optimization from 50L to 500L+ Bioreactors

Executive Summary
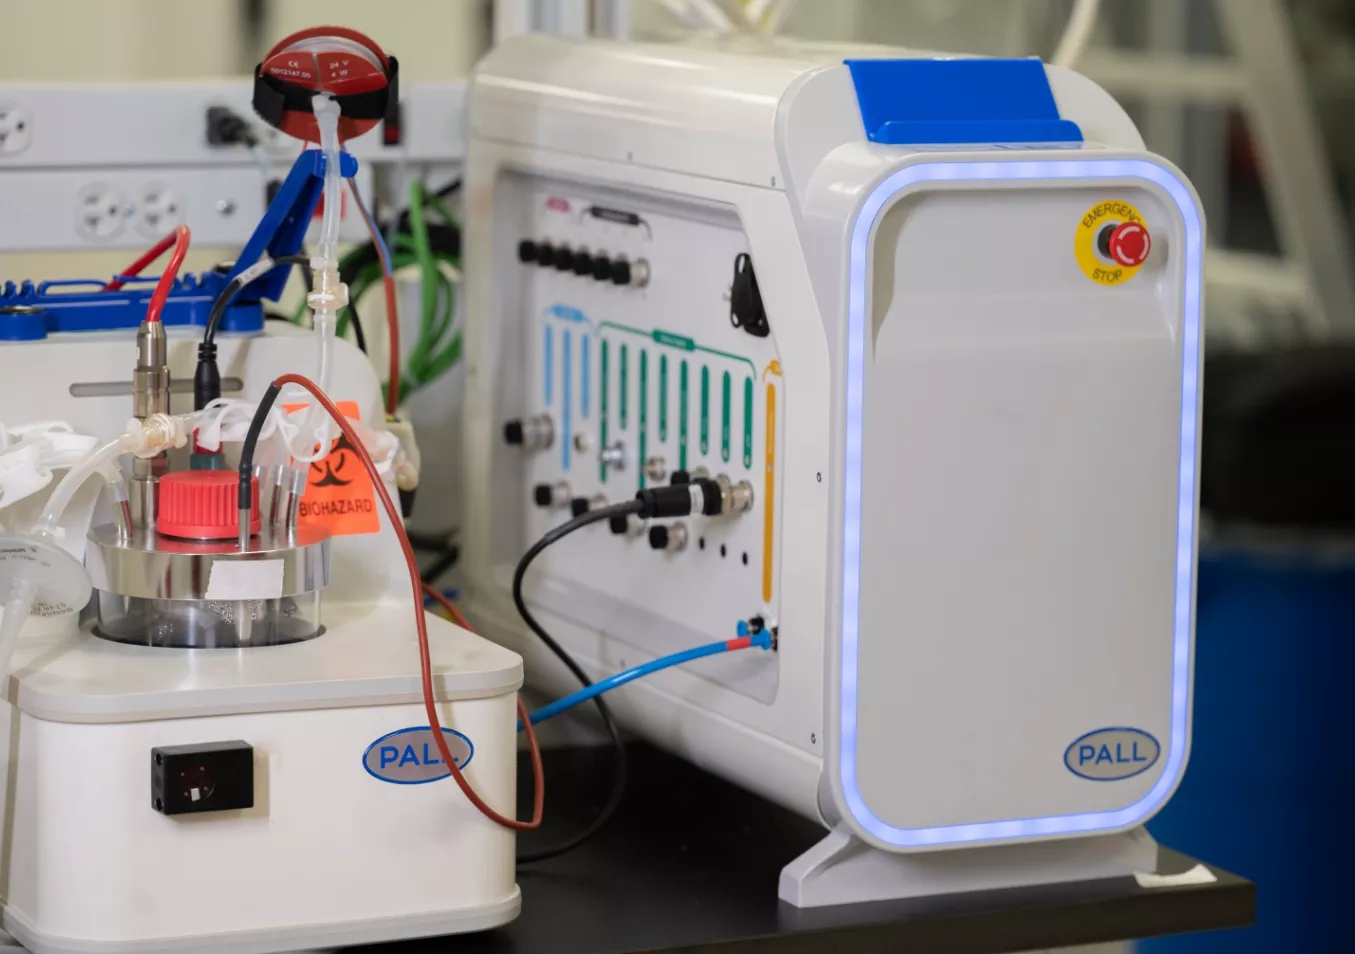
Scaling adeno-associated virus (AAV) production from pilot to clinical-grade volumes requires a dedicated process development strategy that goes beyond simple volumetric increases. This involves re-optimizing key parameters for large-format single-use bioreactors to maintain vector quality, potency, and yield. Areas of focus include transfection efficiency at scale, cell culture media and feed strategies, and downstream purification methods designed for higher volumes and stringent impurity removal. A data-driven approach ensures that the process established at 50L for IND-enabling studies is predictive of performance at 500L and beyond, supporting multi-jurisdictional submissions under ICH guidelines.
Frequently Asked Questions
Q: How does process development for AAV scalable suspension differ between a 50L run for toxicology studies and a 500L run for clinical supply?
A 50L run prioritizes generating representative material for IND-enabling toxicology studies quickly. Process development focuses on vector yield and purity. Scaling to 500L for clinical supply shifts the focus to process robustness, cost of goods, and batch-to-batch consistency. Parameters like transfection reagent sourcing, media consumption, and downstream column cycling become primary optimization targets to establish a locked, commercially viable process.
Q: What are the primary CMC challenges when transitioning AAV production from pilot to large-scale single-use bioreactors?
The main CMC challenges involve maintaining product comparability and consistency. This includes ensuring equivalent transfection efficiency, managing shear stress in larger vessels, and adapting downstream purification to handle significantly higher volumes of lysate and impurities. Analytical assays must be robust enough to detect minor process-related variations in the final product’s defined quality attributes (CQAs).
Q: Can a platform process for AAV suspension culture be adapted for novel or engineered capsids?
Yes, a platform process provides a strong foundation. However, novel or engineered capsids often require specific optimization. Their unique surface properties can affect production characteristics in HEK293 cells, influence their binding affinity to chromatography resins, and alter their stability profile. A tailored process development study is typically required to adapt the platform for a new capsid’s specific biology and chemistry.
Scaling AAV suspension culture from a 50L development scale to a 500L+ clinical production volume is not a linear exercise. The biophysical environment within a large single-use bioreactor presents distinct challenges to cell physiology and viral vector assembly that must be addressed through rigorous process development.
The objective is to establish a robust, reproducible manufacturing process where the defined quality attributes of the vector produced at 500L are directly comparable to the material used in pivotal IND-enabling toxicology studies. This requires a deep understanding of how parameters established in smaller vessels translate to larger geometries.
Key process parameters requiring re-evaluation and optimization include:
* **Transfection Dynamics**: The efficiency of plasmid DNA delivery to suspension HEK293 cells can change with scale. Optimization focuses on mixing speeds, reagent concentration, and the use of scalable transfection reagents to ensure consistent vector genome packaging.
* **Cell Culture Environment**: Maintaining optimal pH, dissolved oxygen, and nutrient levels is more complex in a 500L bioreactor. Feed strategies are adjusted to prevent nutrient depletion and the accumulation of metabolic byproducts that can inhibit cell growth and vector production.
* **Downstream Purification**: Chromatography and filtration steps must be scaled to accommodate a tenfold increase in process volume. This involves qualifying larger columns and membranes and optimizing buffer exchange and viral clearance steps to handle the increased biomass and potential impurity load.
This level of process control is fundamental. As demonstrated in preclinical studies of AAV delivery, what proves feasible in one context does not always translate directly to another. For instance, investigations into intrathecal AAV administration found that delivery methods effective under certain conditions failed to achieve desired outcomes when parameters were shifted to reflect clinical realities (PMID: 32420410). This principle holds true for manufacturing: a process must be built for the intended scale and application from the outset.
Our approach is grounded in this translational foresight. The scientific leadership and core operational team at Franklin Biolabs have a 100% successful IND rate since 2019, a track record established prior to our formal launch in 2024. This experience, honed across our >100,000 sq ft facility, enables us to de-risk the scale-up process, helping sponsors move from candidate to IND within an 18-24 month timeline. Optimizing manufacturing efficiency is a key component of this acceleration. `
`
This deep institutional knowledge in vector production and analytics, combined with a collaborative service model, is integral to navigating the complexities of process scale-up and regulatory submission.
A well-defined and scalable suspension process provides the foundation for a successful clinical program. It ensures a consistent supply of high-quality vector for global trials and eventual commercialization.
For more information on our foundational manufacturing platforms, please see our parent hub page on [Large-Scale AAV Manufacturing and Process Development](/large-scale-aav-manufacturing-and-process-development_5.md).
—

Featured Video: MAKING LIFE-SAVING RESEARCH AFFORDABLE
This video highlights how process optimization and manufacturing efficiency can reduce preclinical development timelines and costs.
This content is for informational purposes. For guidance specific to your therapeutic program, please contact our team for a consultation.